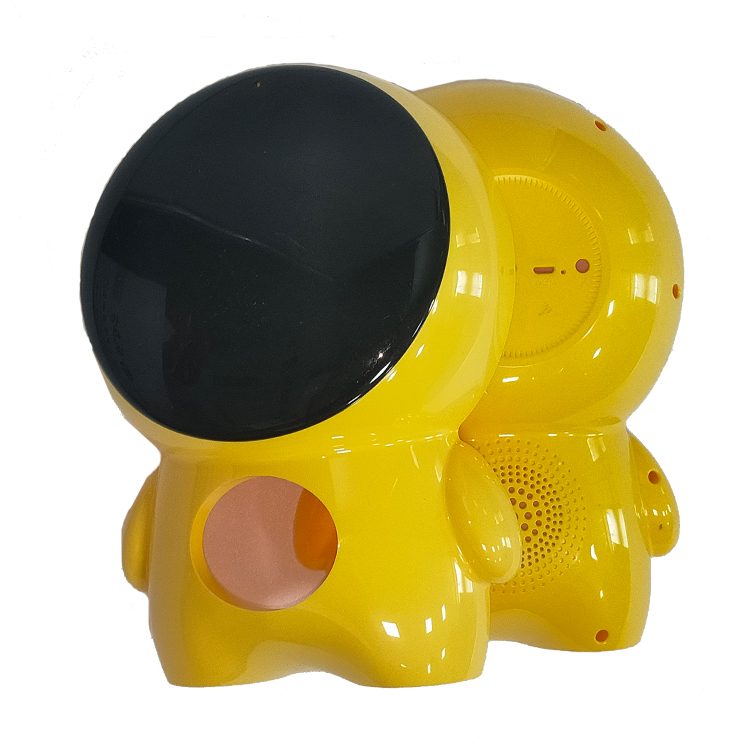
Molded device housing shell
A molded shell with a screen aperture, speaker details and assembly features — tooling, molding and fit handled as one project.
Products · Precision injection parts
Tube, cap and mechanism components molded to the fit that makes a cosmetic package feel expensive in the hand.
Also searched asPrecision injection molded parts · precision moulded components · technical plastic parts · over-molded assemblies
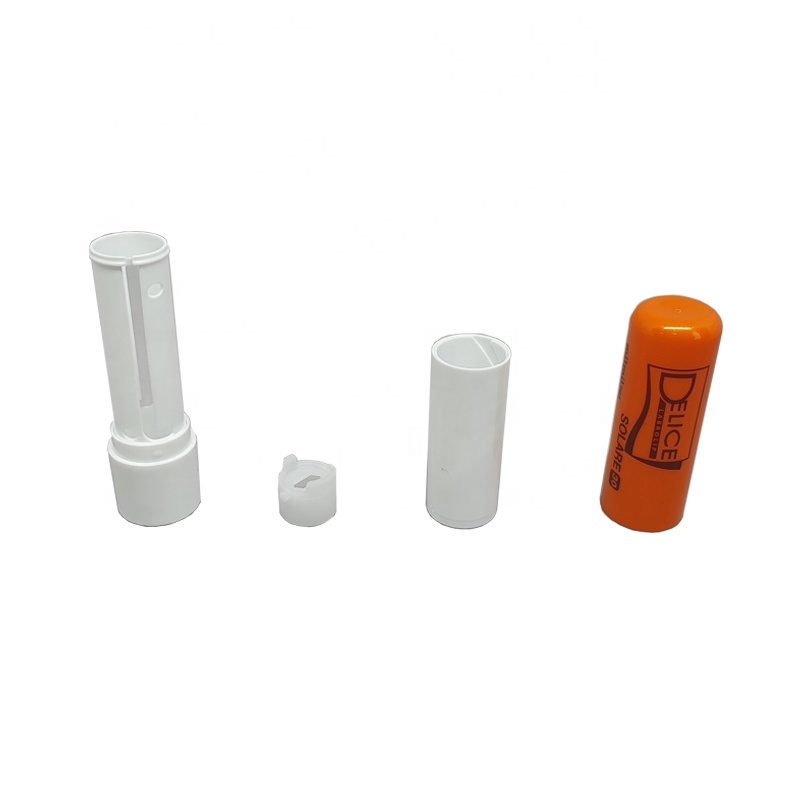
Cosmetic tube components are judged assembled, not individually: the tube has to raise smoothly, the cap has to click with the right resistance, and the surfaces have to stay flawless under the shop lighting of a retail counter. That means tight wall control, symmetric cooling and tight fits between the moulded parts.
For more than 15 years we have manufactured lipstick tubes and cosmetic inner tubes for a well-known European cosmetics brand. The original spec was a 1,000,000-shot mold life; the tools we built were validated at 5,000,000 shots. Parts can ship as components or assembled and packed, ready for your filling line.
Specification
Our standard specification for this type of tooling, confirmed line by line on the mold design approval sheet before machining starts.
| Mold construction | Two-plate, three-plate, hot runner, stack or family — specified per part |
| Cavity count | Single or multi-cavity, sized to annual volume, cycle time and press tonnage |
| Mold steels | P20, 718H, NAK80, S136, hardened H13 / SKD61 cores |
| Mold work tolerance | ±0.01 mm |
| Machine accuracy | Down to 0.001 mm (Yasoda, OKUMA, GF, Makino) |
| Runner | Cold runner, hot runner or valve gate |
| Surface finish | SPI A1–D3, bead blast, leather grain or your texture |
| Cooling | Machined circuits; baffles or bubblers where geometry requires |
| Ejection | Pins, sleeves, stripper plate, lifters, unscrewing or collapsible core |
| Verification | Swiss Hexagon CMM and Zeiss Contura; dimensional report at T1 |
| Molding | 30 presses from 20T to 300T, in the same building |
| Documentation | 2D/3D drawings, steel and component certificates, parameter sheet, spare parts |
| Lead time | Typically 15–30 days of machining after design approval |
| Tool ownership | Yours — the tool is designed to be transferable |
Values above are our standard capability for this class of tool, not fixed figures for a specific project. Cavity count, steel grade, runner type and finish are agreed with you on the design approval sheet before any steel is cut.
Related products · Precision Injection Parts
A molded shell with a screen aperture, speaker details and assembly features — tooling, molding and fit handled as one project.
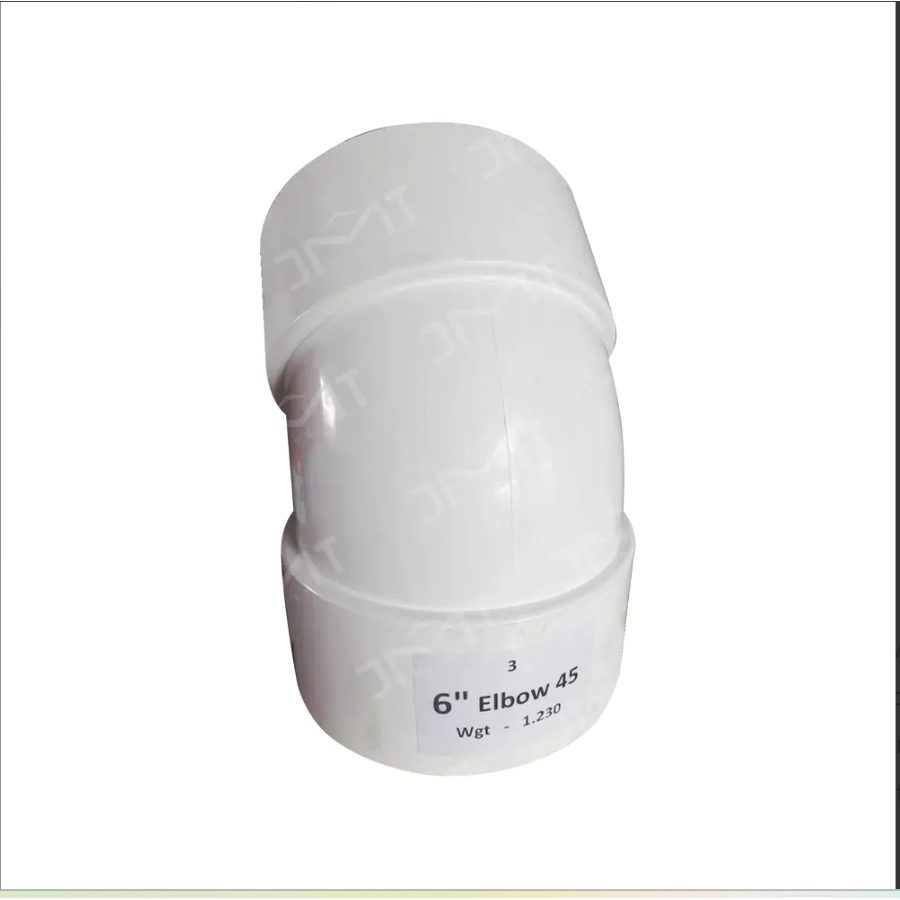
A pipe fitting molded with internal cores and a sealing socket — dimensional accuracy matters far more than appearance.
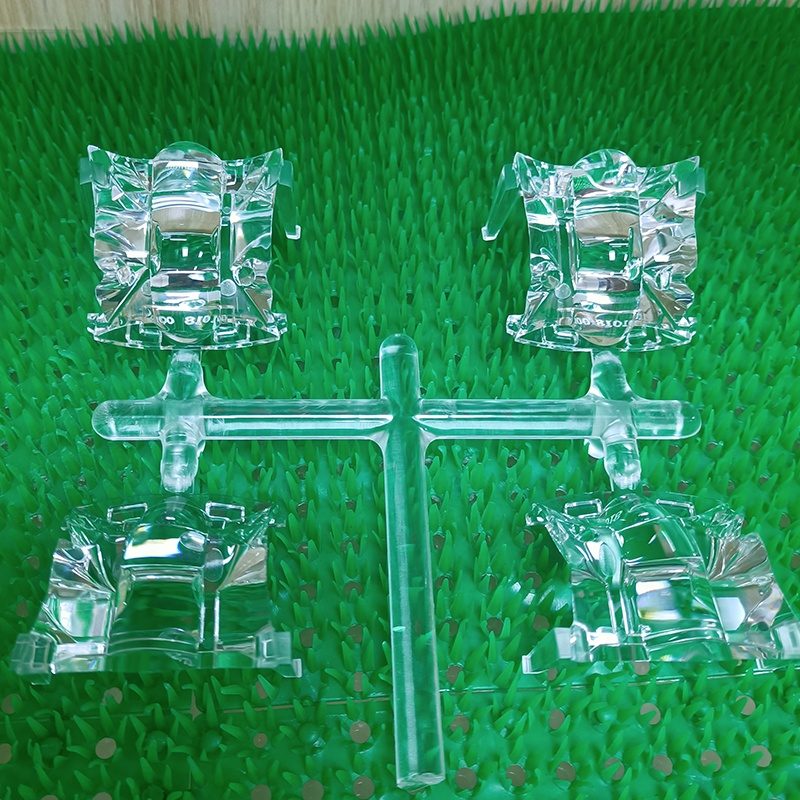
Clear parts to optical standards — the tooling and steel choice do most of the work.
Next step
STEP/IGES/X_T files, the resin, your annual volume and target market are enough to get a mold price, a cycle estimate and the risks we can see — usually in 1–2 business days.