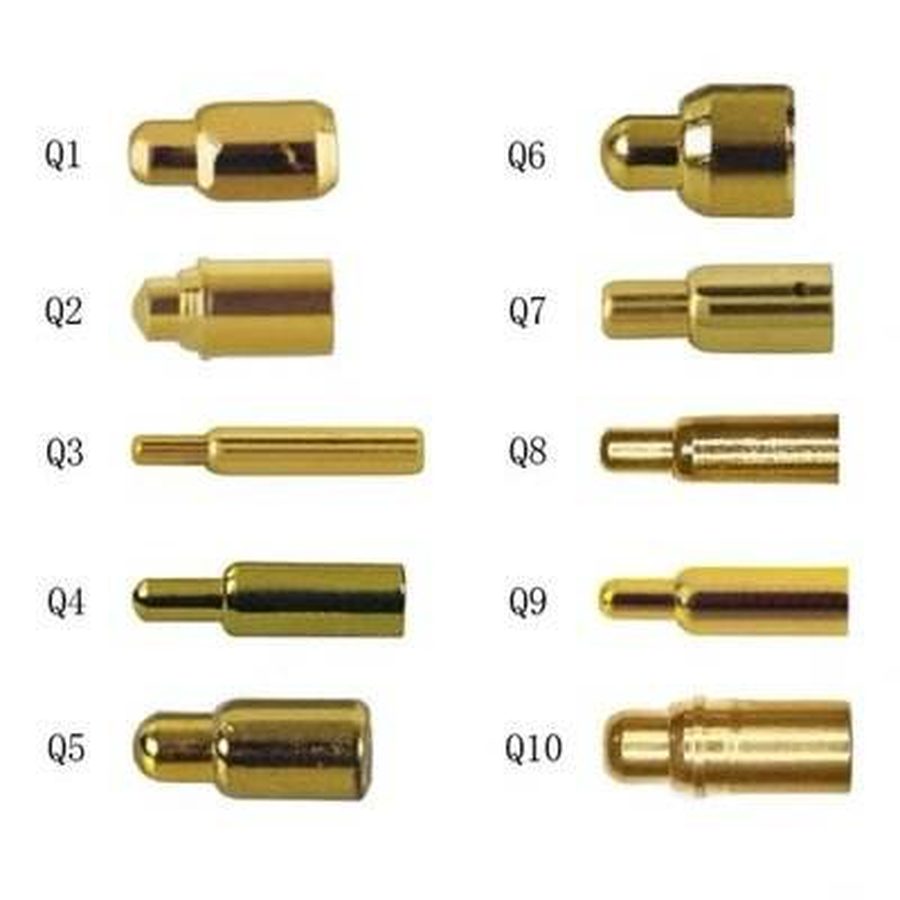
CNC-turned contact pins and terminals
Pins, terminals and bushings turned from bar and measured against one datum.
Products · Metal parts
Single-station dies for tinplate boxes and drawn panels, cut and assembled in our own toolroom and trialled on our own press before they ship.
Also searched asstamping die maker · sheet metal tooling China · tinplate box tool · blanking and forming die · press tool supplier
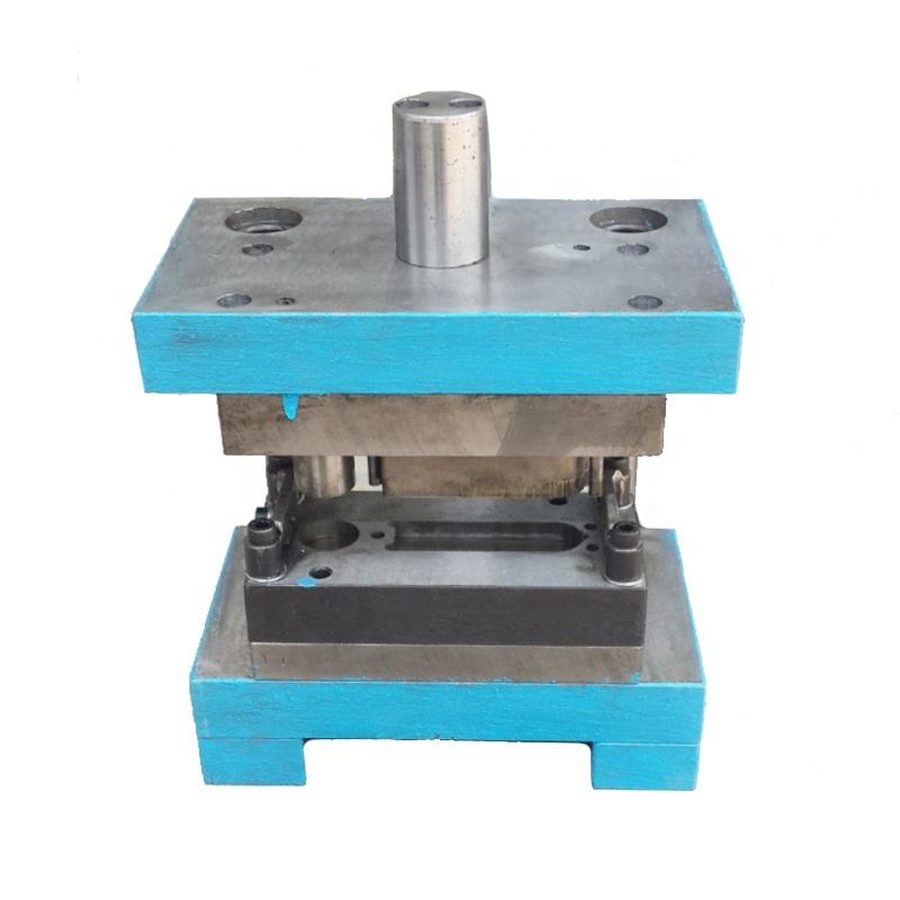
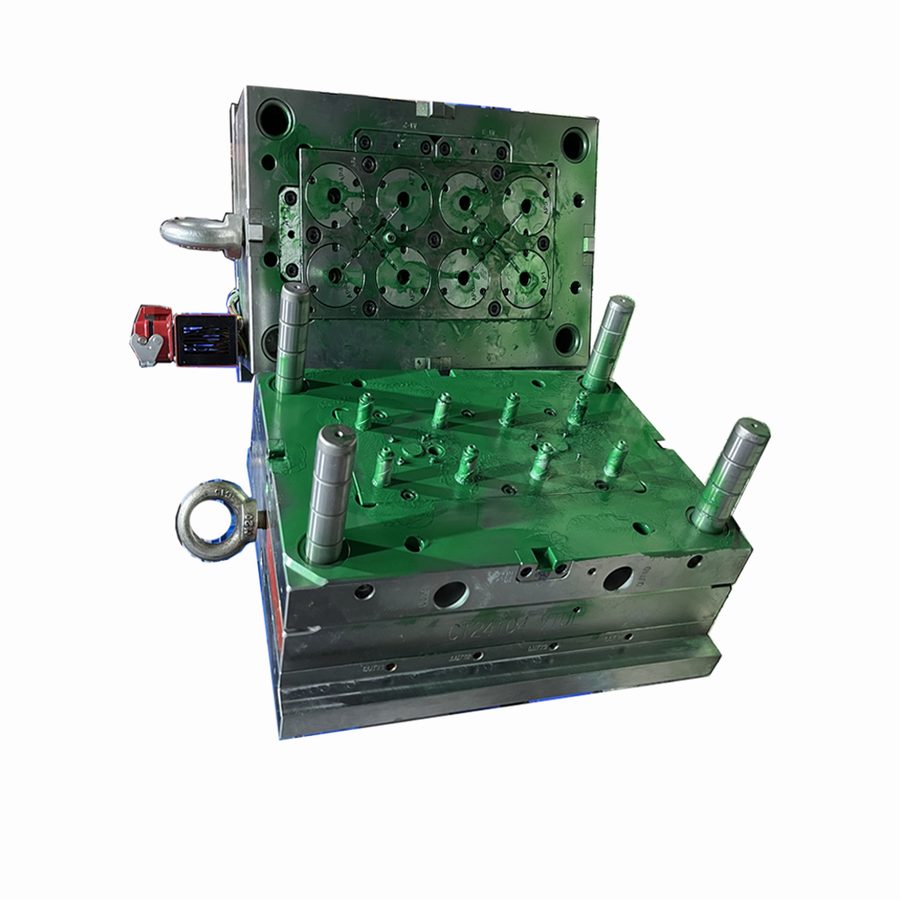
Plastic is not the only thing we tool for. Boxes pressed from tinplate, shallow covers, punched brackets — each needs a stamping die, and the discipline carries straight over: plates machined to ±0.01 mm, punch and die clearance cut on the wire EDM and finished on the sinker, and a guided punch assembly that keeps its alignment across a long run.
The tool in the photograph is single-station: painted base, guide pillars, stripper plate. We build it, run the first parts on our own press and correct clearance and blank development before it ships — so what arrives has already made a sample you can measure against your drawing.
Specification
Standing capability for single-station press tools. Clearance, blank development and the trial run are agreed before plates are cut.
| Tool type | Single-station blanking, forming and drawing dies |
| Manufacturing route | CNC milling of plates; wire-cut EDM for punch and die clearance; sinker EDM for detail |
| Plate tolerance | ±0.01 mm, machine resolution 0.001 mm |
| Guidance | Guide pillars and bushes with a stripper plate on the punch assembly |
| Material | Die steel with hardened punches and wear plates |
| Proving | First parts run on our own press; clearance and blank development corrected before shipment |
| Handover | Sample parts, die drawings and a trial record |
| Maintenance | Spare punches and wear parts quoted with the tool |
Figures are our standing capability for this class of work, not a quotation for a specific job. Material, finish and inspection plan are agreed on the drawing before cutting starts.
Related · Metal parts
Pins, terminals and bushings turned from bar and measured against one datum.
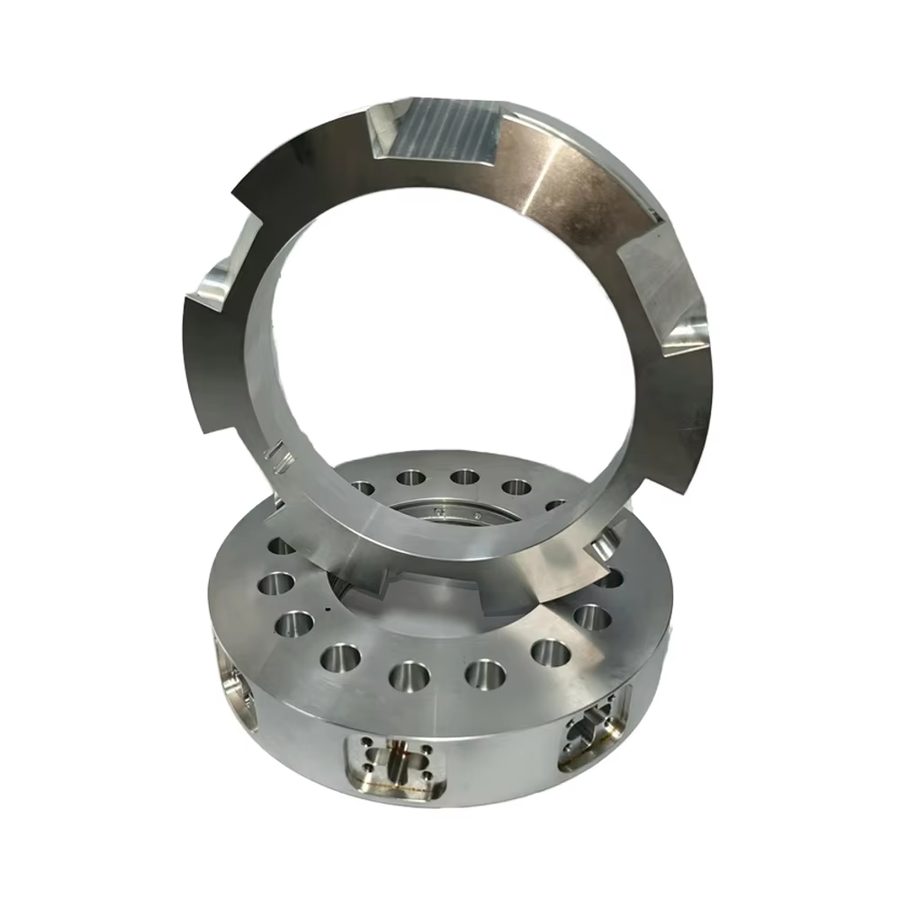
Bored and faced from one datum so the stack assembles without shimming.
Replaceable cores in a common base, sized to volume and press tonnage.
Next step
2D drawing or 3D model, the alloy and the quantity are enough for a price, a lead time and the points we would change before cutting metal.