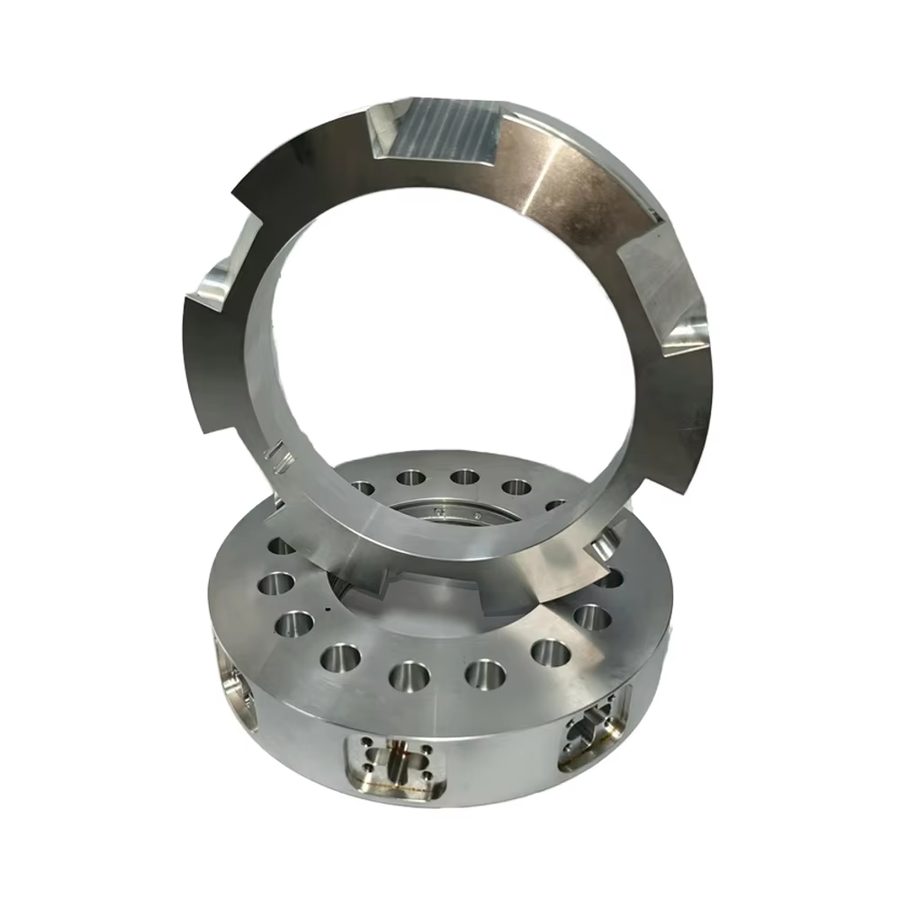
Machined stainless rings and spacers
Bored and faced from one datum so the stack assembles without shimming.
Products · Metal parts
Pins, terminals and spacer bushes turned from bar on lathes we also use for core work — one datum, one inspection, a first-article report with the batch.
Also searched aspogo pin manufacturer · machined contact terminals · brass turned parts · precision turned spacers · CNC machining supplier China
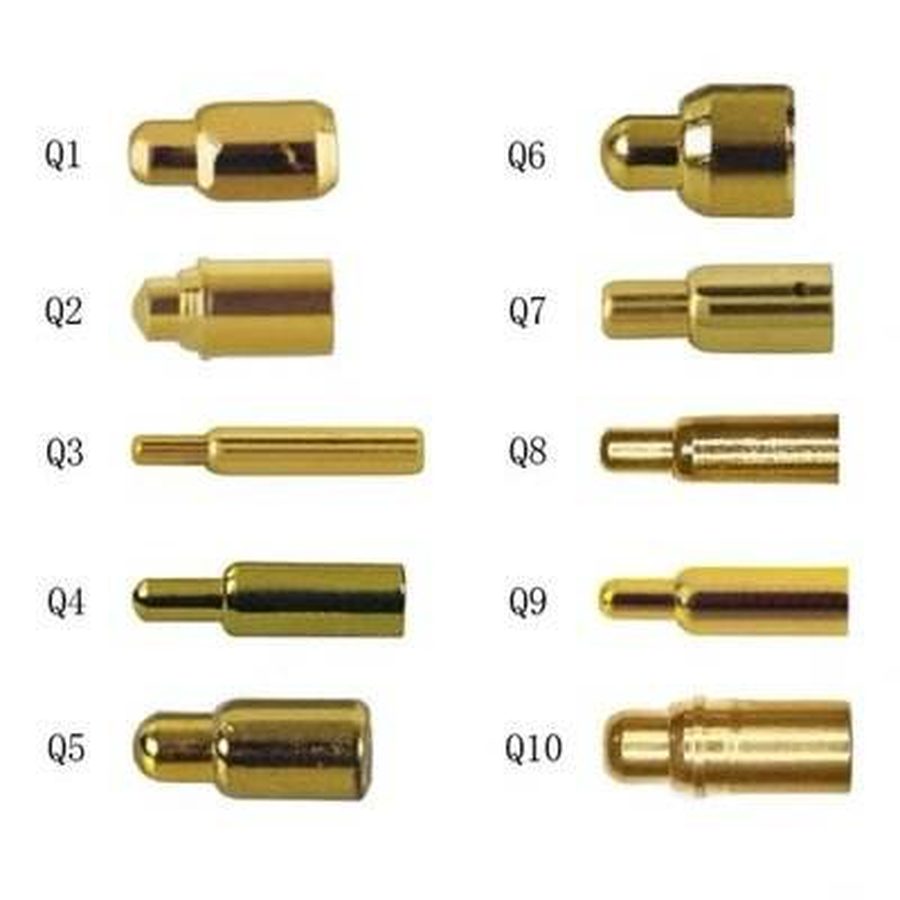
A contact pin is a stack of coaxial features — shank, shoulder, engagement tip. Let any one of them drift off the common axis and the pin binds in its sleeve; the fault surfaces in the field instead of at goods-in. We turn these on CNC lathes standing in the same plant as our molds, so bore, shoulder face and tip radius are cut and then measured against a single datum rather than three.
Alloy, plating and engagement force are settled with you at the DFM stage, before any bar is cut. The alloy sets the spring behaviour, the plating sets the wear life, and together they fix the force you can put in front of your own customer.
Specification
Our standing capability for turned contacts. Alloy, plating and the inspection plan are fixed on your drawing before the first bar is cut.
| Manufacturing route | Turned and milled on CNC centres with drilled and tapped holes; wire-cut and sinker EDM when a die is part of the job |
| Bar stock | Brass, copper alloys, stainless steel, aluminium, titanium |
| Machine resolution | 0.001 mm on Yasoda, OKUMA, GF and Makino centres |
| Drawing tolerance | ±0.01 mm on the features marked critical |
| Finish | As machined, bead blast or polish; plating and anodising to your specification |
| Verification | First article measured on the Swiss Hexagon CMM; dimensional report issued with the batch |
| Order size | Single prototypes through to repeating production orders |
| Paperwork | 2D/3D drawings, material certificate, first-article inspection report |
Figures are our standing capability for this class of work, not a quotation for a specific job. Material, finish and inspection plan are agreed on the drawing before cutting starts.
Related · Metal parts
Bored and faced from one datum so the stack assembles without shimming.
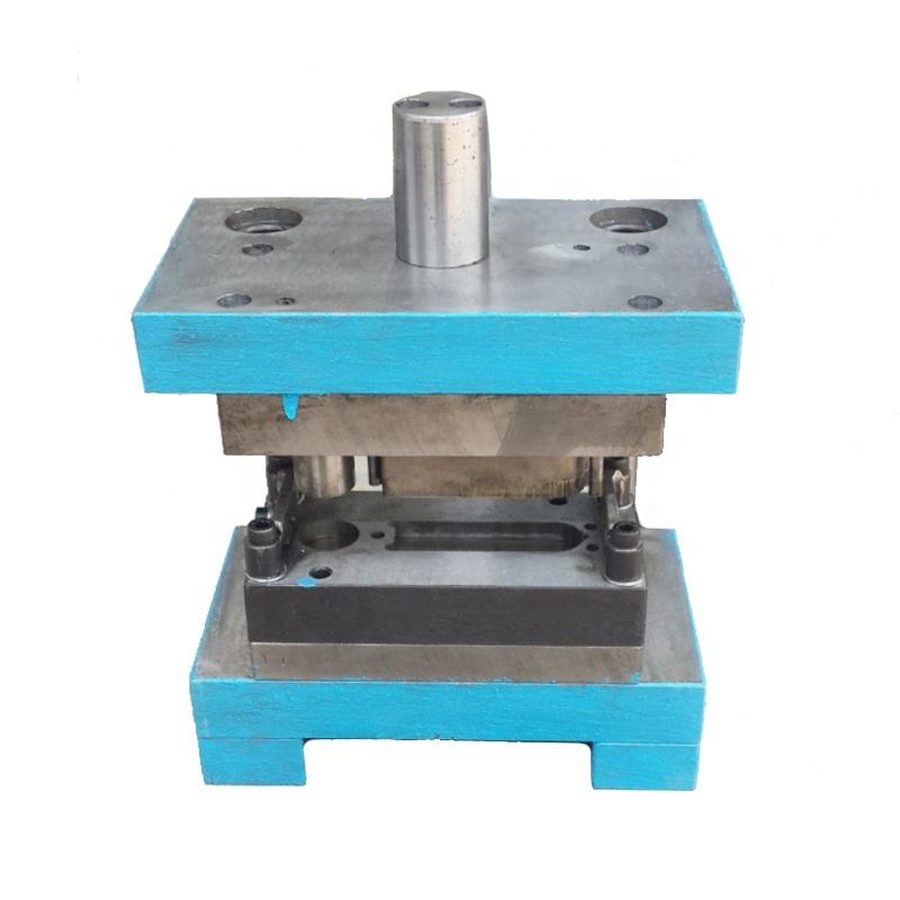
Single-station dies for tinplate boxes and drawn panels, proven on our press before shipment.
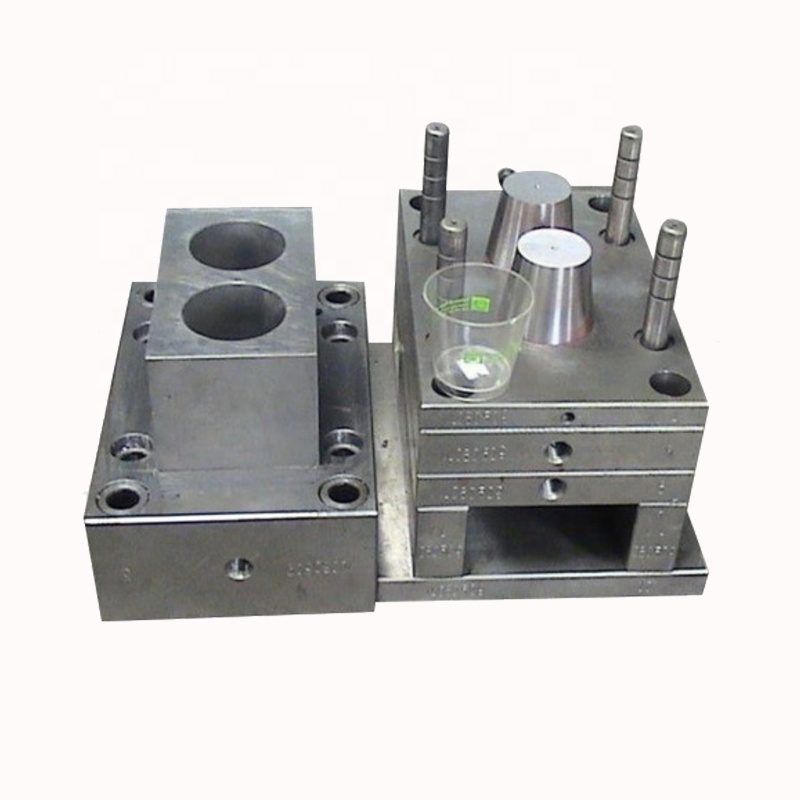
A compact two-cavity tool with balanced cooling and a polished cavity face.
Next step
2D drawing or 3D model, the alloy and the quantity are enough for a price, a lead time and the points we would change before cutting metal.