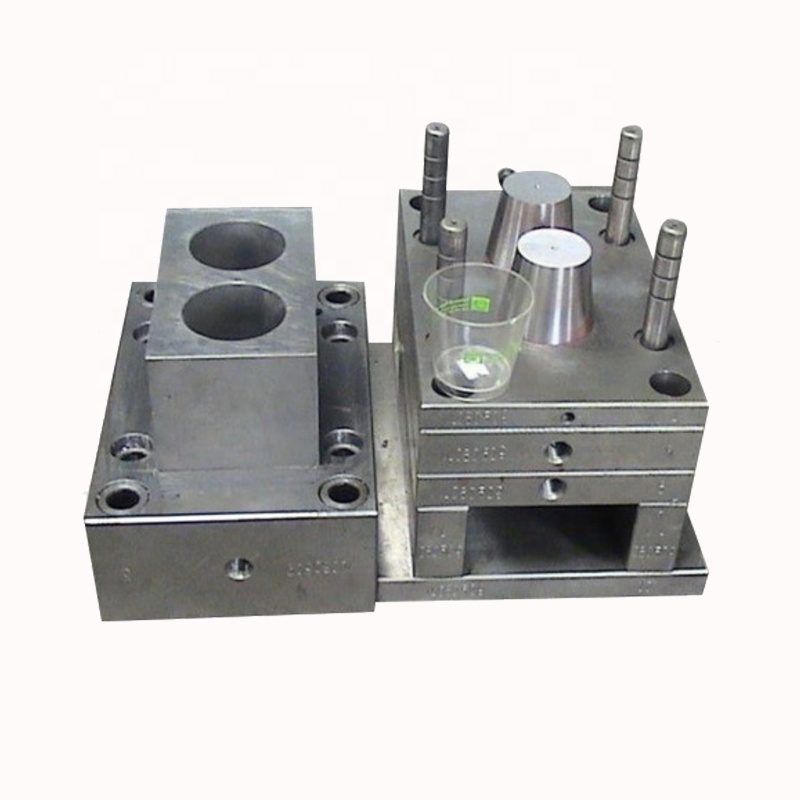
Two-cavity container mold
A compact two-cavity tool for cups and containers, with balanced cooling and a polished cavity finish for a clean visible surface.
Products · Injection mold
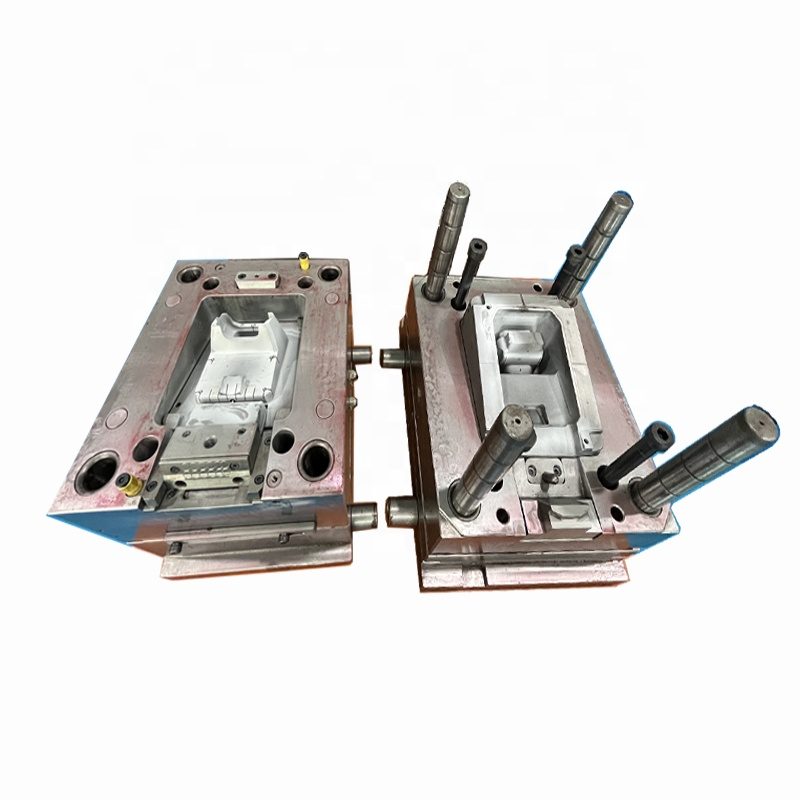
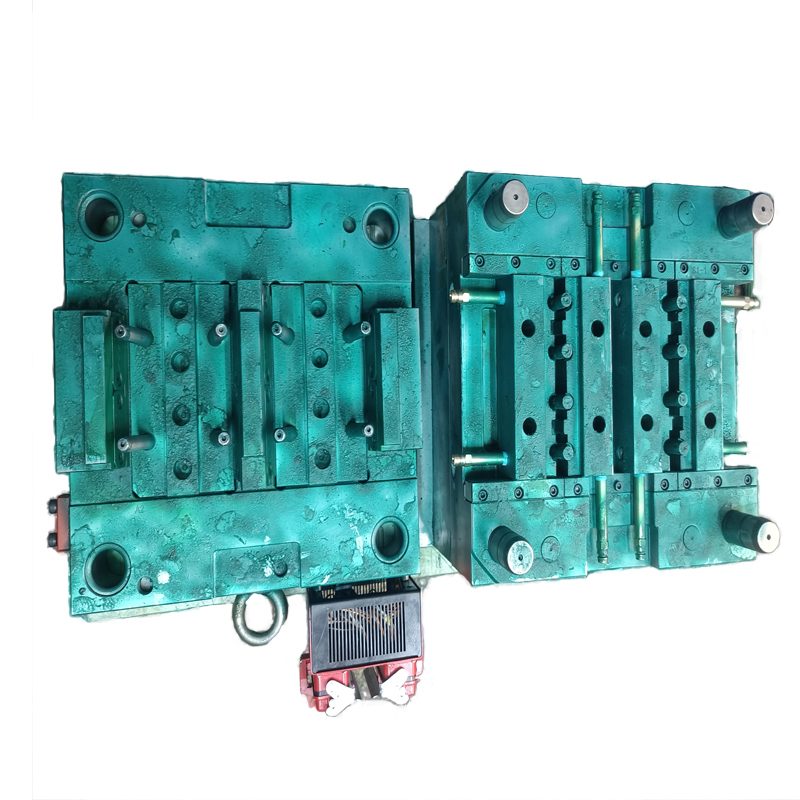
Larger tooling engineered for press handling, lift points and mechanical side action rather than for the bench.
Also searched asInjection mold · injection mould · tooling · toolmaker · mold maker China
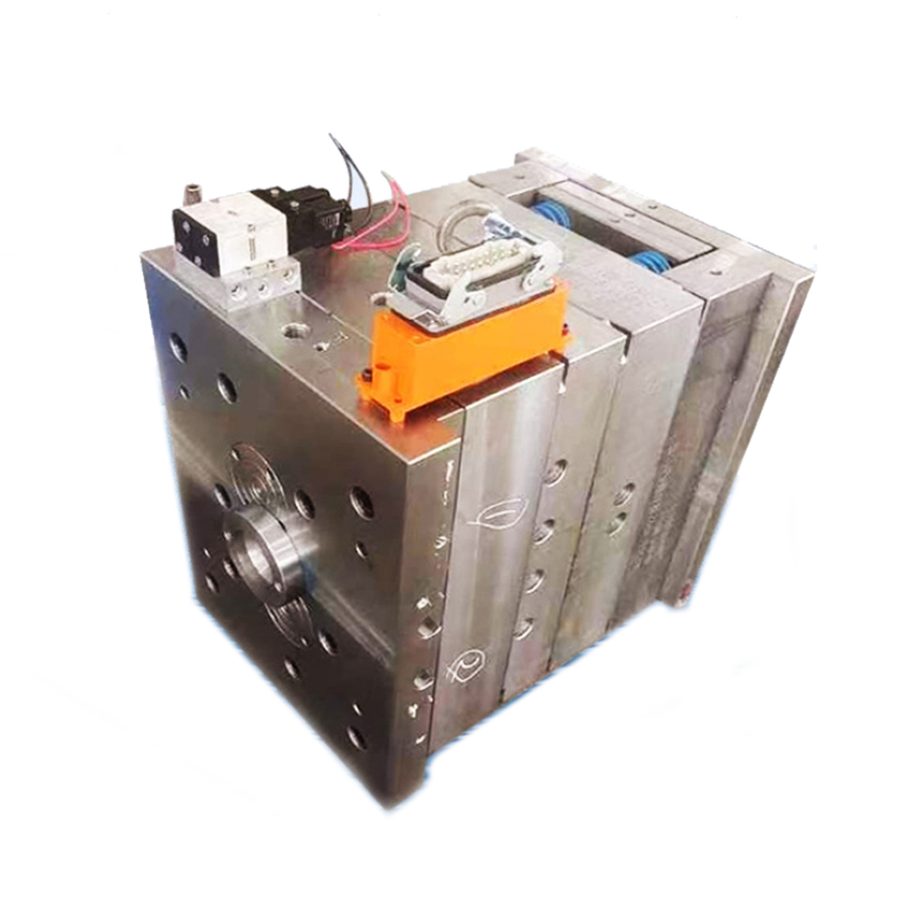
Above a certain size, mold design is as much about handling and press safety as about the cavity: lifting points, plate thickness, clamp slots, cooling manifolds and a mechanism layout that can be assembled inside the working envelope of the machine.
We machine large plates on CNC centres with a 1000 × 580 × 550 mm envelope and grinders sized for the same work, then assemble and trial the tool in-house. Any side action, core pull or hot runner fitted to the tool is commissioned and dry-cycled before the first shot.
Specification
Our standard specification for this type of tooling, confirmed line by line on the mold design approval sheet before machining starts.
| Mold construction | Two-plate, three-plate, hot runner, stack or family — specified per part |
| Cavity count | Single or multi-cavity, sized to annual volume, cycle time and press tonnage |
| Mold steels | P20, 718H, NAK80, S136, hardened H13 / SKD61 cores |
| Mold work tolerance | ±0.01 mm |
| Machine accuracy | Down to 0.001 mm (Yasoda, OKUMA, GF, Makino) |
| Runner | Cold runner, hot runner or valve gate |
| Surface finish | SPI A1–D3, bead blast, leather grain or your texture |
| Cooling | Machined circuits; baffles or bubblers where geometry requires |
| Ejection | Pins, sleeves, stripper plate, lifters, unscrewing or collapsible core |
| Verification | Swiss Hexagon CMM and Zeiss Contura; dimensional report at T1 |
| Molding | 30 presses from 20T to 300T, in the same building |
| Documentation | 2D/3D drawings, steel and component certificates, parameter sheet, spare parts |
| Lead time | Typically 15–30 days of machining after design approval |
| Tool ownership | Yours — the tool is designed to be transferable |
Values above are our standard capability for this class of tool, not fixed figures for a specific project. Cavity count, steel grade, runner type and finish are agreed with you on the design approval sheet before any steel is cut.
Related products · Injection Mold
A compact two-cavity tool for cups and containers, with balanced cooling and a polished cavity finish for a clean visible surface.
A two-plate production mold with mirror-polished cavity and core plates, built for visible Class-A surfaces.
Undercuts solved with cam-driven slides rather than a redesign — for parts with side holes, clips, snap hooks or external features.
Next step
STEP/IGES/X_T files, the resin, your annual volume and target market are enough to get a mold price, a cycle estimate and the risks we can see — usually in 1–2 business days.